"We used 316L stainless steel, which is food-grade" is a phrase often heard in food processing facilities, and it’s only half true. The material is a necessary condition, but it is not sufficient. Hygienic suitability is largely a matter of geometry: a corner where product gets trapped, a pocket that won’t drain, or a rough surface creates a spot that cannot be cleaned, regardless of the material used.
This guide takes the selection of hygienic pumps beyond just the material: it considers the machine’s location, surface roughness, drainage, dead spots, the stresses placed on the pump by CIP/SIP, and pump type selection. We address the chemical aspects of materials in contact with liquids in our material selection guide.
Three zones: Which part of the machine is subject to what?
The hygiene and cleanability requirements for food processing machinery are defined by EN 1672-2. The most useful aspect of the standard is that it addresses the machinery not as a single unit but by dividing it into three zones:
- Food contact area: surfaces that come into direct contact with the product. The strictest requirements apply here.
- Splash zone: Surfaces that the product may splash onto and come into contact with, but does not remain in constant contact with.
- Non-food contact area: Areas that do not come into contact with the product—such as the motor, base, and housing.
Each area has different requirements regarding surface quality, materials, drainage, and accessibility for cleaning. The practical implication is this: a pump does not need to meet food-contact area requirements in their entirety; however, every surface that comes into contact with the food area must meet those requirements. When evaluating a proposal, the question should not be “Is this pump hygienic?” but rather “Which parts come into contact with the food area, and do those parts meet the requirements?”
EN ISO 14159 also addresses the hygiene requirements for machine design. A section of the EHEDG guidelines has been incorporated into both standards; this is the reason why EHEDG-certified equipment is required in the industry.
Surface roughness: Ra 0.8 µm
One of the most concrete numerical requirements in the food industry is surface roughness: a maximum Ra of 0.8 µm. Roughness is expressed as an Ra value in micrometers.
The cause is microbiological: nicks and scratches on the surface create pockets that cleaning solutions cannot reach. Bacteria attach themselves to these areas and begin to form a biofilm; once formed, it becomes difficult to remove with a standard CIP cycle.
There are two points to keep in mind in practice. First, the Ra value is compromised by wear and improper cleaning: an abrasive brush or an unsuitable chemical will, over time, roughen a surface that was initially suitable. Second, weld seams and connection points are the weakest areas of the surface—an unpolished seam will cause problems there, no matter how good the rest of the casing is.
Drainage and dead spot
The second fundamental requirement for the food industry is complete drainability. When the machine is shut down, no product or cleaning solution should remain inside.
The remaining liquid causes two problems: product residue spoils and contaminates the next batch; cleaning solution residue, on the other hand, mixes with the product. For this reason, in a hygienic setup, the pump and piping are installed at an incline, and the drain point is located at the lowest elevation.
A dead leg is a blind end where the fluid does not reach: a closed branch, an unused connection point, or a manometer arm that has been left too long. CIP fluid cannot circulate at a sufficient speed in these areas and therefore does not clean them. In hygienic design, dead legs are either eliminated or kept as short as possible relative to their diameter.
On the pump side, this translates to a design that leaves no gaps or cracks on the surface where the gasket is seated. A standard O-ring groove can become a place where the product gets stuck if the assembly is not hygienic.
CIP and SIP: The Load Placed on the Pump by Cleaning
Hygienic lines are cleaned without being disassembled. During CIP (cleaning in place), hot alkaline and acidic solutions are circulated through the system; SIP (sterilization in place), on the other hand, is performed using steam. For the pump, this means that the machine must handle not only the product but also the cleaning regimen.
In the selection, three separate conditions are listed together:
- Product conditions: temperature, viscosity, particles, cutting precision.
- CIP conditions: alkali/acid concentration and temperature—the elastomer will be exposed to these.
- SIP conditions: steam temperature — this is generally higher than the product and CIP temperatures, and is often the factor that determines gasket life.
A common mistake is to select a pump based solely on the product temperature. The product may be transported at 25 °C, but if the gasket is exposed to steam every day, it is the steam that is the determining factor. We also discuss how temperature defines material limits in our hot service guide.
CIP also imposes a flow condition: the cleaning solution must circulate through the line at a sufficient velocity. This means that the CIP pump must be sized separately—the sizing method is the same as the one described in our guide on TDH and system curves.
What type of pump?
In hygienic lines, the choice of type depends on the product's behavior:
| Product | Suitable for families | Why |
|---|---|---|
| Low-viscosity liquids (milk, fruit juice, water-based) | Hygienic centrifuge | High flow rate, low cost |
| Viscous products (sauce, cream, jam, paste) | Lobe pump | Positive displacement; flow rate is maintained regardless of viscosity |
| Products containing particles (fruit pieces, meat emulsion) | Lobe pump | Wide passage, gentle handling |
| Products highly sensitive to shearing | Lobe/progressing cavity pump | Gentle flow at low speed |
| Intermittent, low flow rate, ease of cleaning is a priority | Peristaltic | The product comes into contact only with the hose |
| Risk of dry running; self-priming required | Air-operated diaphragm | Tolerates dry running |
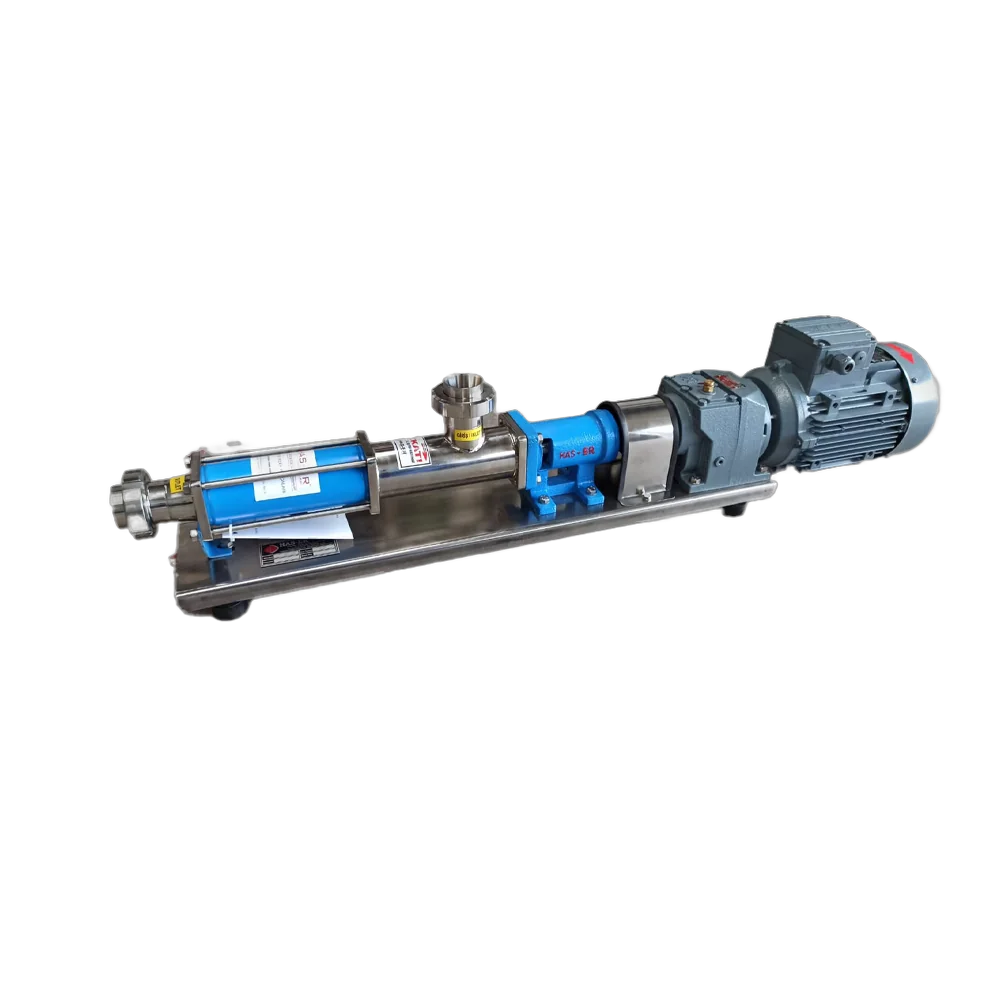
The lobe pump is a classic solution for hygienic processes: the two rotors rotate without coming into contact with each other, and the product is gently conveyed through a large volume. There is an important detail in the lobe series of our gear pump and lobe pump lineup—the casing material is available in GG25 gray cast iron or AISI 316 stainless steel, and only the stainless steel option is considered for food contact. The gears are made of AISI 316 stainless steel; operating parameters range from 20–200 °C, 100–25,000 cP, and 2–14 bar.
With the peristaltic option, the product comes into contact only with the inside of the hose; when the hose is replaced, the wetted surface is completely renewed. This is a significant advantage in terms of cleaning verification. We’ve covered hose lifespan and selection criteria in our dosing pump guide. If dry running and self-priming are required, air-operated double-diaphragm pumps should be considered; within this family, food-grade diaphragm and casing options should be specified.
Elastomer and gasket: the part with the shortest service life
The casing of a hygienic pump lasts for years; the problem almost always stems from the gasket. When selecting a pump, it must meet all three criteria at the same time: the product, the CIP chemical, and the SIP steam.
These three factors rarely combine optimally in a single elastomer; a trade-off is usually necessary. For example, an elastomer that performs well in oily applications may perform poorly in hot alkaline CIP. For this reason, gasket selection is based on all three conditions, and the replacement interval is planned in advance.
We provide the chemical and temperature limits of elastomers in tabular form in our material selection guide. For food contact applications, a declaration of conformity under Regulation (EC) No. 1935/2004 is also required—this is the framework that certifies the material’s suitability for contact with food.
Requesting Documents: What Should You Ask For?
The question "Is it safe for consumption?" is the easiest way to get a "yes" from the seller, but it proves nothing. Instead, three concrete documents are required:
- Declaration of Conformity for Food Contact (1935/2004/EC): For each wet part—the casing, rotor, gasket, and hose—separately.
- Surface roughness value: The Ra value must be specified for surfaces in contact with food.
- Hygienic design reference: Compliance with EN 1672-2 / EN ISO 14159 or EHEDG certification.
Another item that’s often overlooked: lubricant. If there’s a risk that gearbox or bearing grease could contaminate the product, a food-grade lubricant is required.
Symptom → cause → initial examination
| Symptom | Possible cause | Initial inspection |
|---|---|---|
| Poor microbiological results after cleaning | Dead spot or pocket that does not drain | Installation angle; blind branches; gasket seat |
| The problem keeps recurring at the same spot | Surface is rough, biofilm has formed | Ra measurement; weld bead polishing |
| The gasket hardens or cracks quickly | SIP steam exceeds the elastomer’s limit | Steam temperature versus gasket limit |
| The gasket swells, increasing in size | Incompatible with the product or CIP chemical | All three conditions (product/CIP/SIP) |
| Product structure is degrading, particles are dispersing | Shear force is too high — incorrect speed or pump type | Reduce speed; switch to a lobe or progressing cavity pump |
| Cross-contamination in the batch | Residue from the previous batch | Discharge point elevation; drainage design |
| Oil residue on the product | Lubricant leakage | Sealing; food-grade lubricant |
Election Checklist
- Area: Which parts of the pump come into contact with food?
- Product: viscosity, particle size, shear sensitivity, temperature.
- CIP: chemical type, concentration, temperature, and cycle frequency.
- SIP: Steam temperature and duration—these factors often determine the gasket selection.
- Surface: Is the Ra value specified for surfaces in the food contact area?
- Drainage: Is the installation sloped, and is there a drain at the lowest point?
- Dead spots: Are there any blind branches or unused openings?
- Documents: Has a 1935/2004/EC declaration been obtained for each wet part?
- Lubricant: If there is a risk of contamination, is the lubricant food-grade?
- Dismantlability: Do the time and tools required for maintenance comply with the production plan?
Frequently Asked Questions
Does 316L stainless steel mean it's food-safe?
No, that alone is not enough. Material is a necessary condition, but hygienic suitability also depends on geometry: surface roughness, complete drainability, the absence of dead spots, and accessibility for cleaning. A pocket made of the right material but that doesn’t drain is a spot that cannot be cleaned.
Where does Ra 0.8 µm come from?
This is the maximum surface roughness value specified for the food industry. The goal is to prevent the formation of grooves that cleaning solutions cannot reach; bacteria adhere to rough surfaces and form biofilms. Simply meeting this value at the outset is not enough—wear and improper cleaning will degrade the surface over time.
What exactly is a "dead leg"?
A dead end where the fluid cannot reach: a closed branch, an unused connection point, or a measurement arm left longer than necessary. Since the CIP solution cannot circulate at a sufficient speed in these areas, cleaning does not occur. In hygienic design, dead ends are either eliminated or kept as short as possible.
How should I choose a gasket?
By considering all three conditions together: the product, the CIP chemical, and the SIP steam. A common mistake is selecting the pump based solely on the product temperature; even if the product is transported at 25 °C, if the gasket is exposed to steam every day, the determining factor is the steam. There is generally no single elastomer that performs best under all three conditions; compromises are made, and the range of variation is planned from the outset.
Which pump is best for viscous products?
Positive-displacement family. A centrifugal pump loses its performance as viscosity increases; a lobe pump, on the other hand, maintains flow rate and gently handles viscous and particulate products. For products that are highly susceptible to shearing, the speed is reduced. When low flow rate and easy cleaning are priorities, the peristaltic option stands out.
What documents should I ask the seller for?
Three specific requirements: a declaration of conformity for food contact under Directive 1935/2004/EC for each wet part, a specified Ra value for surfaces in the food area, and a reference to hygienic design (EN 1672-2 / EN ISO 14159 compliance or an EHEDG certificate). If there is a risk of contamination, also request confirmation of the lubricant’s food-grade compatibility.
Summary
Choosing a hygienic pump starts with the material, but it doesn’t end there. The three-zone classification in EN 1672-2 prompts the right question: Which parts of the pump come into contact with the food area? For those parts, a surface roughness of Ra 0.8 µm, complete drainability, and the absence of dead spots are required.
The choice of pump type is determined by the product’s characteristics—lobe pumps for viscous and particulate products, hygienic centrifugal pumps for low-viscosity products, and peristaltic pumps for low flow rates and easy calibration. The choice of container, however, is often determined not by the product but by SIP steam; a selection made without considering all three conditions together will be short-lived.
If you provide us with your product’s specifications, your CIP/SIP regimen, and the required flow rate, we can work together to determine the appropriate type and material combination. You can review our stainless steel and lobe pump lines or get in touch with us for technical support.